TIG Welding Aluminum Problems and Their Fixes
TIG welding aluminum problems like sooty beads, porosity, cracking and tungsten trouble, with the causes, the fixes, and the electrode sizes and tip prep that keep aluminum welds clean.

On this page
Top picks at a glance
As an Amazon Associate I earn from qualifying purchases.
- 1
 YESWELDER 110V Tungsten Electrode Sharpener9.7/10View on Amazon
- 2
 YESWELDER TIG Welding Tungsten Electrode Red Tip9.6/10View on Amazon
- 3
 ARCCAPTAIN TIG Tungsten, TIG Welding Tungsten9.6/10View on Amazon
- 4
 TIG Welding Tungsten Electrodes 2% Lanthanated9.4/10View on Amazon
An aluminum joint that looked ready can still come out gray and sooty, with a bead that sits on the surface instead of wetting in. The puddle wanders, the tungsten balls up or dips into the metal, and the weld that should have been clean needs grinding out and a fresh start. This guide covers tig welding aluminum problems and the fixes that sort them, from electrode choice and tip prep to the cleaning and fit-up habits that keep aluminum welds sound.
This guide links to our product roundups, where WeldGearLab gets a commission on purchases made through links on this page, and your price stays the same. Read our affiliate disclosure.
YESWELDER 110V Tungsten Electrode Sharpener
A wired 110V tungsten sharpener with 4 sizes, 3 angles and 6 speeds, a cut-off slot and a dust cover, with a 1 year warranty stated.
Pros
- Grinds 0.040, 1/16, 3/32 and 1/8 inch electrodes
- 3 angles: 15, 22.5 and 30 degrees
- 6 speeds with a cut-off slot for damaged tips
- 1 year warranty stated in the listing
Cons
- Wired 110V only, so it needs mains power at the bench
- Diamond wheel service life is not stated
- Size and weight are not stated
- Cutting off a damaged tip shortens the electrode each time
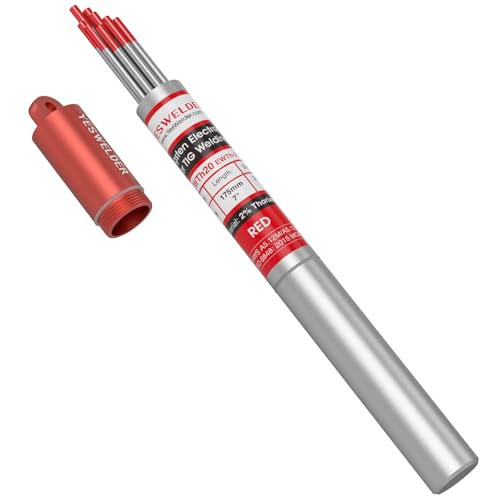
YESWELDER TIG Welding Tungsten Electrode Red Tip
A 10-pack of 1/8 inch by 7 inch red WT20/EWTh-2 tungsten in a sealed aluminum tube, with AWS A5.12M/A5.12:2009 conformance stated.
Pros
- 10 pieces of 1/8 inch tungsten, 7 inches long
- Sealed aluminum tube stated to prevent oxidation
- Dual-open tube design for easy access
- AWS A5.12M/A5.12:2009 conformance stated
Cons
- 1 size only, so no smaller diameter for thin work
- No warranty term is stated
- No stated guidance for aluminum or AC use
- Listing states no angle or prep guidance for the tip
ARCCAPTAIN TIG Tungsten, TIG Welding Tungsten
A 10-piece red tungsten pack in 1/16 and 3/32 inch sizes, 7 inches long, that states AWS A5.12M/A5.12:2009 conformance and lists DC work on copper, nickel, titanium alloys and stainless steel.
Pros
- 2 sizes in a pack: 5 pieces of 1/16 inch and 5 of 3/32 inch
- States AWS A5.12M/A5.12:2009 and DIN EN 26848 conformance
- Listing claims fast arc striking and a low burn off rate
- Vacuum packing stated, with 100% traceability claimed
Cons
- Listed for DC applications, which does not match AC aluminum work
- No warranty term is stated
- Only 7 inch length stated, with no other length option
TIG Welding Tungsten Electrodes 2% Lanthanated
A 10-pack of 2% lanthanated blue tungsten, 3/32 inch by 7 inches, listed as a versatile electrode that re-ignites arcs easily.
Pros
- 2% lanthanated, blue WL20 type
- 10 pieces of 3/32 inch by 7 inch
- Listing claims reliable arcs and clean, solid welds
- Listed as versatile across many welding types
Cons
- No standard or certification is stated
- No warranty term is stated
- 1 size only in the pack
- Listing gives no angle, prep or aluminum guidance
TIG Welding Aluminum Problems: What Goes Wrong
Aluminum welds go wrong in a few repeatable ways, and most trace back to the surface, the electrode, or the fit-up rather than the machine. A dirty bead with black soot points to contamination on the metal or the tungsten. Porosity, small holes in a finished bead, points to gas or dirt trapped in the puddle. Cracking points to a joint that moved as it cooled. Tungsten trouble, a tip that balls, splits or dips, points to the wrong electrode type or a tip ground the wrong way.
Side by side
| Gear Score | Electrode type | Sizes in the pack | |
|---|---|---|---|
| YESWELDER Tungsten Sharpener 110V | 9.7/10 | Sharpener, 110V wired | 0.040, 1/16, 3/32, 1/8 in |
| YESWELDER Red Tungsten 1/8 10-Pack | 9.6/10 | Red WT20/EWTh-2 | 1/8 in x 7 in, 10 pieces |
| ARCCAPTAIN Red Tungsten 10-Pack | 9.6/10 | Red tungsten, WT20/EWth-2 per title | 1/16 and 3/32 in x 7 in, 10 pieces |
| Pur.Tungsten Lanthanated 3/32 10-Pack | 9.4/10 | 2% lanthanated, blue WL20 | 3/32 in x 7 in, 10 pieces |
The sharpener leads on range of sizes and angles, plus a stated 1 year warranty. The red tungsten packs follow, with the YESWELDER 1/8 inch pack ahead on packaging. The lanthanated pack trails on stated standards and warranty, though its 2% lanthanated type suits a wide range of work.
The Gear That Fixes These Problems
Each problem above has a gear answer: the right electrode type and size for the joint, and a sharpener that keeps the tip ground the same way.
Electrode Choice for Aluminum
Electrode type matters more on aluminum than on steel, because the wrong type balls, splits or dips and puts tungsten in the puddle. The YESWELDER red pack states WT20 thoriated tungsten, while the Pur.Tungsten pack states 2% lanthanated blue WL20, listed as versatile across many welding types. Read the listing before buying: the ARCCAPTAIN listing names WT20/EWth-2 in its title and WL20/EWLa-2 in its bullets, so the stated type is unclear. The ARCCAPTAIN pack also lists DC applications, which suits steel and stainless work.
Tip Prep and Angles
A tungsten tip ground clean and even starts the arc the same way each time. The YESWELDER sharpener grinds 0.040, 1/16, 3/32 and 1/8 inch electrodes at 15, 22.5 and 30 degrees, with 6 speeds and a cut-off slot for damaged tips. Its dust cover holds the tungsten particles made during grinding, and the double-sided diamond wheel grinds from both sides. Keep the angle the same across a job and regrind the tip the moment it dips or balls.
FAQ for welders
Why does my aluminum TIG weld come out black and sooty?
Soot on an aluminum bead usually means contamination reached the puddle, from a dirty joint, a dipped tungsten tip, or filler rod stored open to shop dust. Clean the joint and the filler before welding and regrind any tungsten that touched the puddle.
Why does my tungsten ball up or split on aluminum?
A tungsten tip balls or splits when the electrode type does not suit the work. Red thoriated tungsten suits DC work, as the ARCCAPTAIN listing states, while 2% lanthanated tungsten is listed as versatile across many welding types. Match the electrode to the listing, grind the tip to a clean point, and regrind the moment the tip dips or balls.
What tungsten size should I use for aluminum?
The packs in this guide cover 1/16, 3/32 and 1/8 inch diameters, all 7 inches long. Thinner joints suit the smaller diameters, while thicker joints suit the larger ones. Pick the diameter the joint calls for.
What angle should I grind my tungsten to?
The sharpener in this guide offers 15, 22.5 and 30 degree angles, and the right angle depends on the joint and the arc shape the welder wants. What matters most is grinding the same angle each time. A cut-off slot handles damaged tips, so a chipped tip gets cut back and reground instead of welded with.
Why do my aluminum welds crack?
Cracking in aluminum usually follows a joint that moved as it cooled, a poor fit-up that left a gap, or contamination in the puddle. Clamp the joint so it cannot move, close gaps before welding, and clean the metal and the filler. If cracking keeps showing up on the same kind of joint, change the fit-up and the cleaning routine.
Related: tig welding aluminum problems, the best TIG welder guide, how do you TIG weld aluminum, and best TIG collets for aluminum. Also see the TIG welders hub.