Tapping Types: Taper, Plug and Bottoming Taps Explained
Taper, plug and bottoming taps cut the same thread in different ways: which one starts, which one cuts deeper, and which one finishes a blind hole.

On this page
Top picks at a glance
As an Amazon Associate I earn from qualifying purchases.
- 1
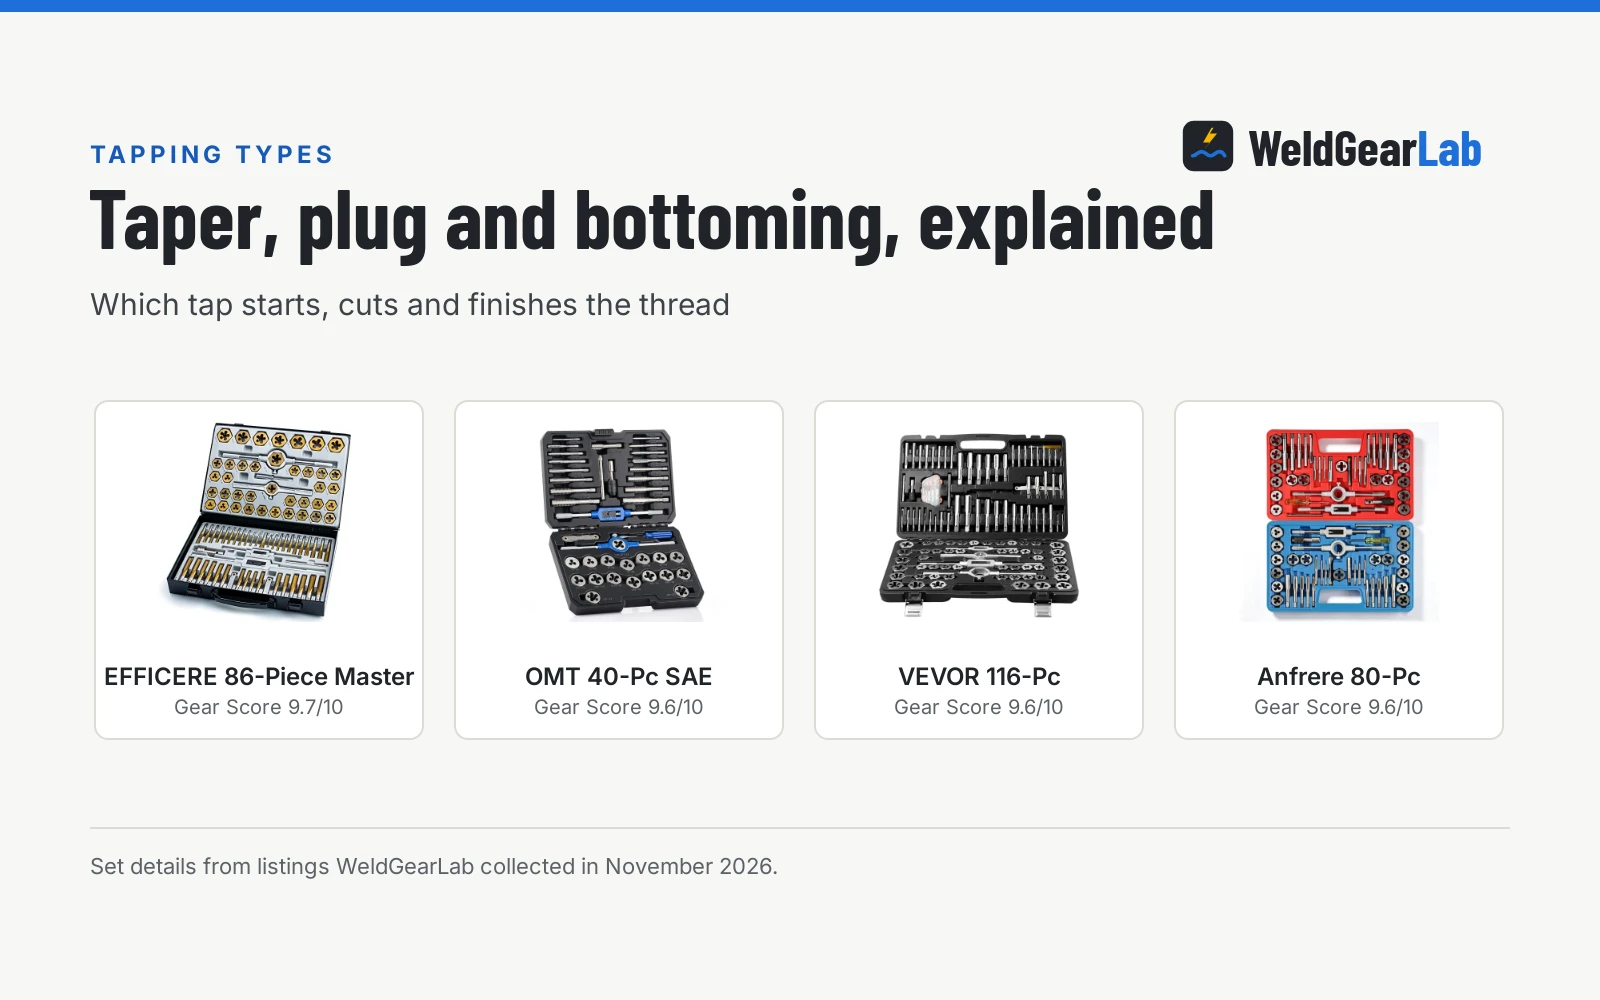
 86-Piece Master Tap and Hex Die Set9.7/10View on Amazon
- 2
 OMT SAE Tap and Die Set, Thread Repair and Cutting9.6/10View on Amazon
- 3
 VEVOR Tap and Die Set 116 Pcs Metric and SAE Size9.6/10View on Amazon
- 4
 Anfrere 80pcs Tap and Die Set for Cutting External9.6/10View on Amazon
A stripped bolt hole stops a repair cold. The bolt spins, the joint will not hold, and the part has to come off the machine again. Tapping types are the way back: a tap cuts or restores the internal thread in a hole, and the type of tap decides how the cut starts, how it tracks, and how far it reaches.
This guide links to our product roundups, where WeldGearLab gets a commission on purchases made through links on this page, and your price stays the same. Read our affiliate disclosure.
86-Piece Master Tap and Hex Die Set
An 86-piece master set in SAE and metric, with titanium-coated HSS taps and dies, hex dies and a metal case.
Pros
- Covers SAE #4 to 5/8 in and metric M3 to M16, coarse and fine
- Hex dies work with wrenches and sockets for added leverage in tight spaces
- Titanium-coated HSS, which the maker claims lasts 3 times longer than a normal ground finish
- Two thread pitch gauges and three tap handles in the box
Cons
- No warranty term is stated
- Metric range stops at M16
- SAE range stops at 5/8 in
- Sorting through 86 pieces takes time when one size is needed
OMT SAE Tap and Die Set, Thread Repair and Cutting
A 40-piece SAE set with 34 taps and dies, three tap wrenches and a thread pitch gauge, in heat-treated GCr15 bearing steel.
Pros
- 1 year warranty, the only stated term in this guide
- 34 taps and dies in the sizes the maker calls the most commonly needed
- Three tap wrenches and a die wrench in the box
- Blow-molded case keeps each piece in its place
Cons
- SAE sizes only, so metric threads need another set
- Range stops at 1/2 in
- Fewer pieces than the other sets here, so odd sizes may be missing
- Tap ends run 1/5 to 2/5 inches, so other wrenches may not fit the taps
VEVOR Tap and Die Set 116 Pcs Metric and SAE Size
A 116-piece set with 51 taps and 51 dies in metric and SAE, HRC56 bearing steel, plus 5 extractors.
Pros
- 116 pieces, the largest set here
- 51 taps and 51 dies across metric and SAE
- 5 extractors in the box for broken fasteners
- HRC56 bearing steel with 800℃ heat treatment and double polishing
Cons
- No warranty term is stated
- At 13.23 lb it is the heaviest set here
- 116 pieces take sorting to find one size
- Tap wrenches cover m3-m12 and m6-m20, so sizes outside those ranges need another wrench
Anfrere 80pcs Tap and Die Set for Cutting External
An 80-piece SAE and metric set with 17 taps and 17 dies on each side, GCr15 bearing steel hardened to 60 HRC.
Pros
- 80 pieces split evenly: 40 metric and 40 standard
- Taps and dies hardened to 60 HRC
- 2 tap wrenches, 2 die wrenches and 2 T-handle tap wrenches in the box
- Two thread gauges, SAE and metric
Cons
- No warranty term is stated
- Metric range stops at M12
- No extractors in the box for broken screws
- Finding one size means sorting the full 80-piece case
The three tapping types
Taper, plug and bottoming taps all cut the same thread, but each one leads the cut differently. The lead is the tapered end of the tap, and a longer lead starts easier and tracks straighter, while a shorter lead cuts threads closer to the bottom of the hole. Pick the type by the hole: whether it goes all the way through, whether it is blind, and whether the thread is new or a repair.
Taper tap. The taper tap has the longest lead, so it starts with the least effort and follows the hole straight. Use it to start a new thread. It leaves threads uncut at the bottom of a blind hole, so it is not the tap that finishes one.
Plug tap. The plug tap sits in the middle, with a shorter lead than a taper tap. It starts a thread with more effort than a taper tap, and it cuts closer to the bottom of a blind hole. For through holes and for threads that are already started, the plug tap is a sound choice.
Bottoming tap. The bottoming tap has almost no lead, so it cuts threads nearly to the bottom of a blind hole. It needs a thread that is already started, so run a taper or plug tap first, then switch to the bottoming tap for the last turns.
Read more in what tapping is and how taps cut threads.
Which tapping type for which hole
- New thread in a through hole. A taper tap cuts the full thread as it passes through the hole.
- New thread in a blind hole. Start with a taper tap, follow with a plug tap, and finish with a bottoming tap so the thread runs close to the bottom.
- Damaged thread. Chase it with the matching tap, which follows the old thread and clears burrs.
- Thread that must run to the bottom. The bottoming tap runs the thread closest to the bottom of the three.
Clamp the work before the tap goes in, wear eye protection, and keep gloves away from a tap turning under power. A tap is brittle, so turn it steady, back it off to break the chip, and use tapping fluid. Our best tapping fluid guide covers five picks for clean threads.
The four sets side by side
| Product | Pieces | Sizes | Steel | Warranty | Gear Score |
|---|---|---|---|---|---|
| EFFICERE 86-Piece Master | 86 | SAE #4 to 5/8 in, metric M3 to M16 | HSS, titanium coating | Not stated | 9.7/10 |
| OMT 40-Pc SAE | 40 | SAE #4 to 1/2 in | GCr15 bearing steel | 1 year | 9.6/10 |
| VEVOR 116-Pc | 116 | Metric and SAE | Bearing steel, HRC56 | Not stated | 9.6/10 |
| Anfrere 80-Pc | 80 | Metric M3 to M12, SAE | GCr15 bearing steel | Not stated | 9.6/10 |
The table ranks the four sets by Gear Score, with the EFFICERE set on top for range and the OMT set close behind on the strength of its stated warranty. All four cut internal and external threads, and all four carry the wrenches and gauges the job needs.
Tap and die sets for every tapping type
Cutting a thread takes the right tap for the hole, and the set has to cover the thread sizes the job calls for, with the wrenches and gauges to run it. The four sets below are ranked by Gear Score.
FAQ for welders
Which tapping type starts a new thread?
A taper tap starts a new thread with the least effort. Its long lead centers the tap in the hole and cuts gradually, so it tracks straight. Follow it with a plug tap, and a bottoming tap when the hole is blind.
Can a plug tap finish a blind hole?
A plug tap cuts closer to the bottom than a taper tap, but it still leaves threads uncut at the bottom of a blind hole. For a thread that must run close to the bottom, finish with a bottoming tap after the plug tap has started the thread.
Do I need all three tapping types?
Not for every job. A plug tap handles through holes and threads that are already started, and a taper tap starts new threads and chases damaged ones. Add a bottoming tap when blind holes need threads that run close to the bottom.
What is the difference between a tap and a die?
A tap cuts internal threads inside a hole, and a die cuts external threads on a rod or bolt. Tap and die sets carry both, so one kit covers thread repair on bolts and nuts alike. Match the set to the sizes the job calls for, SAE or metric.
Can a tap repair a damaged thread?
Yes, when the damage is light and the tap matches the thread. Run the matching taper tap through the hole with tapping fluid, turning steady and backing off to clear chips. When threads are stripped past repair, a thread repair kit or a larger fastener is the next step. See our thread repair kit guide.
How do I pick a tap and die set?
Match the set to the thread sizes the job calls for, SAE or metric, and check the range it covers. Look for the steel and hardness the maker states, the wrenches and gauges in the box, and a warranty term in writing. The four sets above cover SAE only, metric and SAE together, and piece counts of 40, 80, 86 and 116.
Related: what tapping is, best tapping fluid, thread pitch gauge chart, drilling and tapping chart, and the metal fab tools hub.